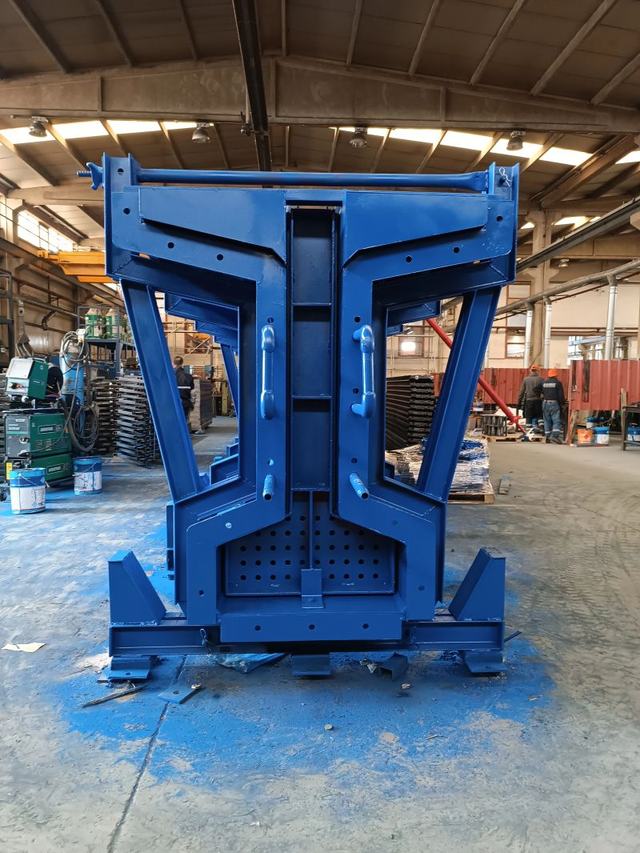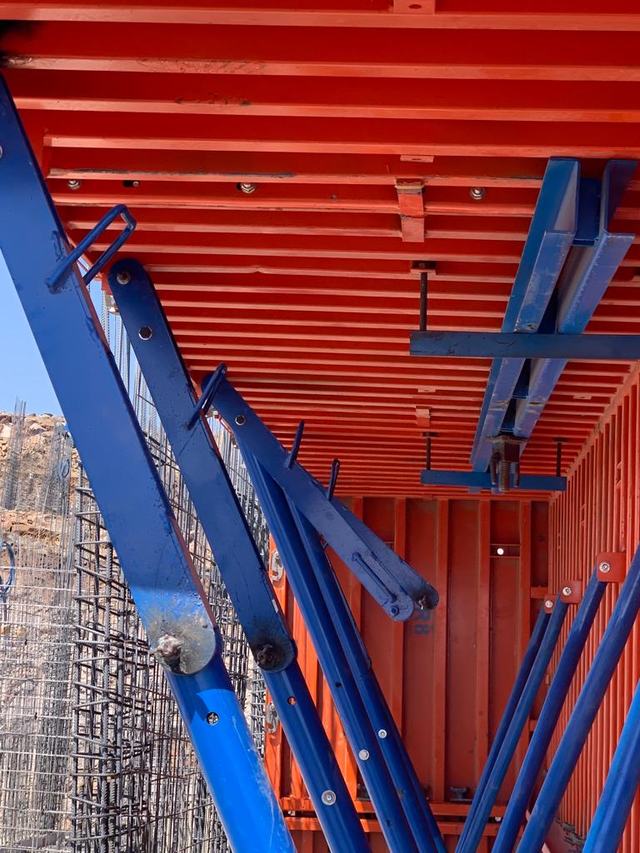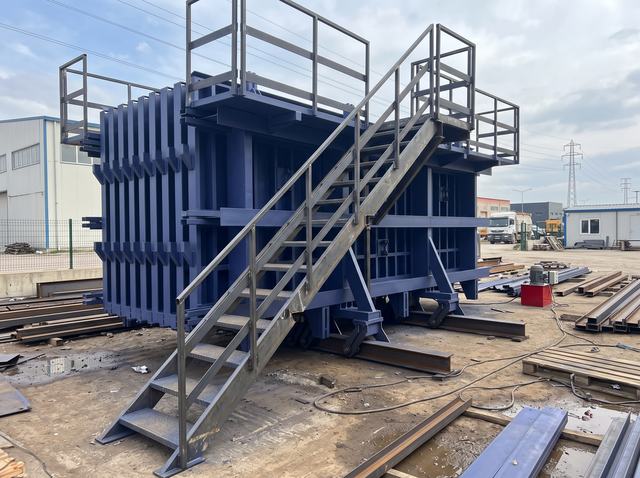
A box culvert is a rectangular reinforced concrete structure carrying water under roads, railways and irrigation lines. It is produced in two ways: cast in situ or precast in a plant. The formwork differs between them.
In-situ culvert formwork
Preferred on long runs and where the section varies. The form works as an inner core plus outer panels:
- The inner core must fold inward after casting; otherwise it cannot be stripped. Hinges or wedge mechanisms are provided at the corners for this.
- The outer panels form the side walls; tie rods connect the two sides.
- The system advances on rails; once a bay has been cast and has set, the form is drawn forward.
- Bay length is usually 6–12 m, set by crane capacity and concrete output.
The critical point is the retraction allowance of the inner core. If it is too small, the form locks into the concrete, and forced stripping damages both the surface and the mould.
Precast culvert mould
Used in series production at repeating dimensions. Here the mould is fixed and the element moves:
- The outer form has four hinged panels
- The inner core folds inward by a hydraulic or screw mechanism
- Concrete is placed from above and compacted by mould-mounted vibrators
- After curing, the element is lifted by its anchors
With steam curing, the cycle comes down to 12–24 hours.
Why taper is needed
In both types a slight taper of 0.5°–2° is given to the inner faces. The reason is simple: on a perfectly vertical face, friction between concrete and steel makes stripping impossible. The taper lets the form break away in the first few millimetres; the rest comes easily.
The taper is kept small enough not to compromise the design section and is always given in the stripping direction.
Inputs that govern the design
| Input | What it determines |
|---|---|
| Internal dimensions (width × height) | Core size |
| Wall and slab thickness | Outer form opening, tie spacing |
| Bay length | Mould length, transport |
| Fresh concrete pressure | Panel plate, stiffening |
| Section variability | Need for filler pieces |
| Production volume | Mechanism type (screw / hydraulic) |
| Crane capacity | Piece weight and splitting |
Common problems
The core jams — insufficient taper or missing release agent. Check the agent first; if it persists, the taper must be increased.
Honeycombing at corners — concrete cannot reach internal corners. Add corner chamfers, increase vibration, reduce aggregate size.
Sagging mid-slab — the core's top deck is not carrying the slab load. Support trusses are fitted inside the core.
Grout leakage at joints — panel joints without seals. Leaking grout both marks the surface and builds up in the mould.
Level differences between bays — the rail track is not true. Rails are checked by levelling before each pour.
In situ or precast?
| In situ | Precast | |
|---|---|---|
| Section variability | Flexible | Must be uniform |
| Line length | Economical over long runs | Depends on haul distance |
| Weather | Affected | Not affected |
| Erection speed | Slow | Very fast |
| Joints | Fewer | A joint at every unit |
| Crane | Small is enough | High capacity |
Precast comes out ahead on short crossings and accessible sites; in-situ casting suits long runs with varying sections.
In short
In culvert moulds, everything comes down to stripping: the core retraction mechanism, the taper and joint tightness. Get those right and the mould runs for hundreds of cycles without trouble.
PRODUCT GROUPS IN THIS ARTICLE
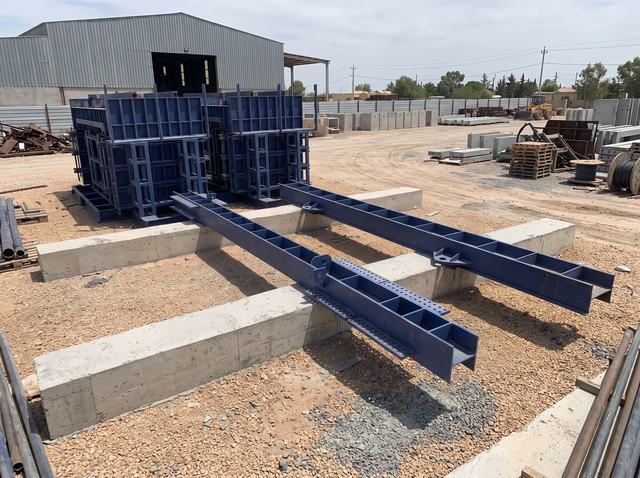
CULVERT MOULD
Inner and outer mould set for box culverts and channel elements.
VIEW IRRIGATION CHANNEL MOULDIRRIGATION CHANNEL MOULD
Steel mould for irrigation channels and open channel elements.
VIEW PIPE AND CONDUIT MOULDPIPE AND CONDUIT MOULD
Concrete pipe and conduit moulds for stormwater and sewerage lines.
VIEWLet us work out the right formwork configuration for your project.
REQUEST A QUOTE